11 Gauge Steel: 3.0mm Thickness, Springback & Warping Guide
- Share
- publisher
- Tianjin Yuantai Derun steel pipe manufacturing group Ltd.
- Issue Time
- Apr 15,2026
Summary
11 gauge steel = 3.0mm. Learn why it springs back 1-3°, warps during laser cutting, and how stress-relieved ERW tubing prevents fabrication cracks.
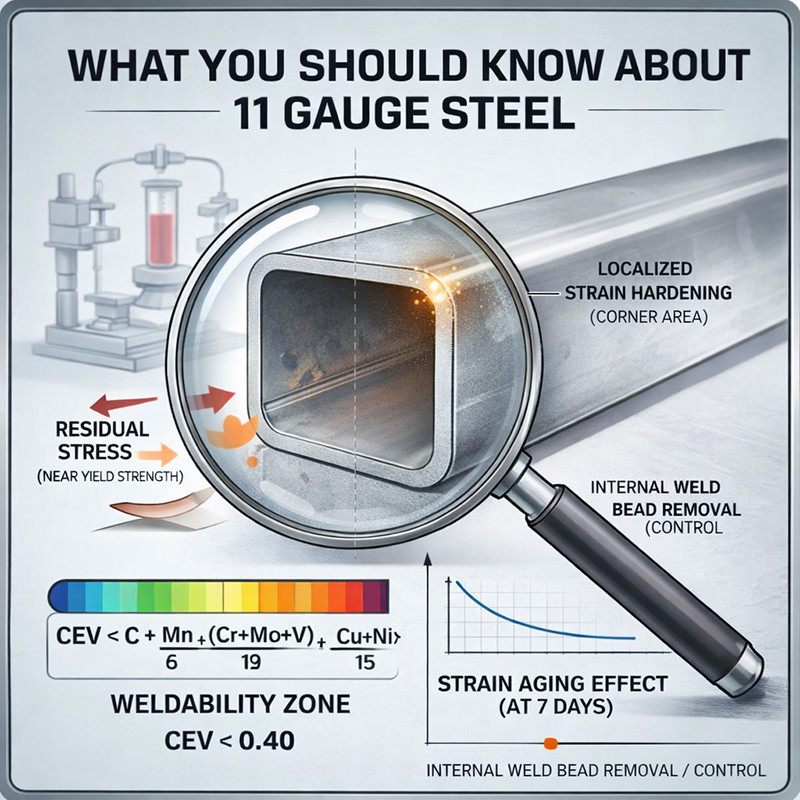
11 Gauge Steel: 3.0mm Thickness, Springback & Warping Guide
Key Takeaways
- 11 gauge steel = 3.038 mm (≈3.0 mm) for carbon steel.
- It springs back 1°–3° after bending — operators must over-bend.
- Laser-cut warping is caused by residual stress release, not bad cutting.
- A smooth internal weld bead (ERW scarfing) prevents stress-crack failures.
- Specify stress-relief + CEV when sourcing, not just "11 gauge".
"11 gauge steel" refers to a nominal wall thickness of 3.0 mm (0.1196 in) carbon steel tubing — a size that sits between light sheet and heavy plate, making it a workhorse for solar racks, automotive frames, and structural SHS.
That positioning gives 11 gauge steel a temperament of its own. Bend it, and it springs back. Laser-cut it, and it can twist. Drill it, and the bit burns out. These aren't defects — they're the three hidden traits of 3.0 mm steel, and knowing them is the difference between a masterpiece and a logistical nightmare.
The "Muscle Memory" (The Spring back Factor)
In precision manufacturing, 11 gauge steel is notorious for its "memory." When you bend a 3.0mm plate to a 90-degree angle, the atoms inside are engaged in a silent tug-of-war.
The Reality: The moment the press brake releases, the steel "remembers" its flat shape and kicks back by 1° to 3°.
The Human Touch: Unlike thinner gauges that are easily tamed, 11 gauge requires an experienced operator who understands Over-Bending. If your supplier doesn't account for the specific yield strength of that batch, your "square" tubes will arrive slightly trapezoidal, ruining your assembly fit-up.
Per ASTM A500, typical yield strength of Grade B is 317 MPa — the higher the yield, the larger the over-bend angle required.
The "Hardened Heart" (Strain Hardening)
11 Gauge steel often undergoes significant cold-forming to reach its final shape. While this makes the steel stronger (increasing its yield strength), it comes at a cost: Ductility.
We call this "Work Hardening." If a factory "over-works" the 3.0mm strip to achieve a razor-sharp corner radius, the steel becomes stressed and brittle. Have you ever had a drill bit smoke and burn out while trying to pierce a 3.0mm tube? That’s not a bad drill bit—that’s the steel’s "hardened heart" fighting back. High-quality manufacturing ensures a balance, giving you strength without sacrificing the ability to weld or drill.
CEV (Carbon Equivalent Value) above 0.45 needs pre-heating before welding to avoid cold cracking.
The "Silent Bat tle" (Residual Stress Release)
This is the most "mysterious" phenomenon in steel processing. Every 11 Gauge tube is a pressurized vessel of internal energy. During the rolling and welding process, immense stress is locked inside the metal.
The "Snake" Effect: If you take a 6-meter length of 11 gauge SHS and perform a longitudinal slit, the tube will often twist or splay open instantly.
For engineers designing complex frames, understanding Stress Relief is vital. If you plan on heavy laser-cutting or asymmetrical welding, you must choose steel that has been "tuned" during the cooling process. Otherwise, your straight frame will look like a literal snake by the time it hits the assembly line.
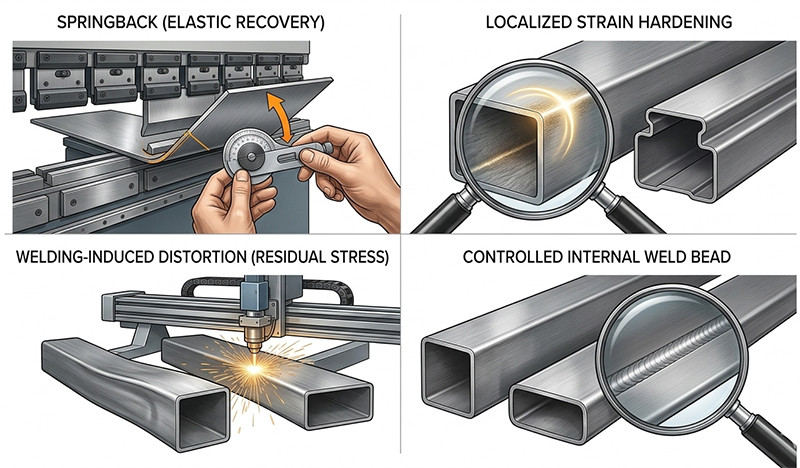
Stress-relief annealing at 550–650 °C removes 70–90% of locked-in stress.
When 11 gauge steel is ERW, a "scar" or bead is formed inside the tube. While the outside looks smooth and polished, the Internal Scarfing tells the real story.
The 0.2mm Secret: T he Internal Weld Bead
If a manufacturer is careless and leaves a jagged internal bead—or worse, cuts too deep into the 3.0mm wall while trying to remove it—they create a Stress Concentration Point. Over time, vibration and load will cause the tube to crack along this "invisible line." A premium 11 gauge tube should have an internal seam so smooth it’s almost felt rather than seen.
| Gauge | Thickness (mm) | Typical use | Bending difficulty |
| 12 gauge | 2.6 | light frames | Low |
| 11 gauge | 3.0 | structual SHS,racks | Medium(springback) |
| 10 gauge | 3.4 | heavy frames | High |
11 Gauge vs 10/12 Gauge: Which Should You Specify?
Specify 11 gauge (3.0 mm) when your frame needs more rigidity than 12 gauge provides but doesn't justify the extra weight and cost of 10 gauge (3.4 mm). It's the default for solar mounting racks, automotive sub-frames, and medium-load structural SHS where weldability and flatness beat brute thickness. Weight-critical? Drop to 12 gauge (2.6 mm). Load-critical? Step up to 10 gauge.
Why Thickness is Only Half the Story
At 3.0mm (11 Gauge), steel is a living material. It has a "temper" that reacts to heat, a "memory" that resists bending, and "internal stress" that waits for the right moment to release.
When sourcing for your next project—whether it's solar mounting racks, automotive frames, or architectural skeletons—don't just ask for "11 Gauge." Ask your partner about their Springback compensation, their CEV (Carbon Equivalent Value) for weldability, and their Stress-Relief protocols.
True quality isn't just measured by a caliper; it's measured by how the steel behaves long after it leaves the mill.
FAQ
Q1: How Thick Is 11 Gauge Steel In Millimeters?
For standard carbon steel, 11 gauge is approximately 0.1196 inches, which translates to 3.038 mm. However, keep in mind that galvanized and stainless steel have slightly different gauge charts. In the structural steel industry, it is commonly referred to as 3.0mm thickness.
Q2: Why Does My 11 Gauge Steel Tube Warp When I Laser-Cut It?
This is caused by the release of residual stress. During the cold-forming and welding processes at the mill, 11 gauge steel builds up internal tension. When you cut into the tube—especially with large or asymmetric holes—that locked-in stress is suddenly released, causing the metal to twist or warp. Purchasing stress-relieved steel can prevent this.
Q3: Is 11 Gauge Steel Hard To Bend?
While it is manageable with a standard press brake, 11 gauge steel is notorious for elastic recovery. Because of its specific thickness and yield strength, the steel will naturally try to return to its flat shape. Operators usually need to "over-bend" the metal by 1 to 3 degrees to achieve a perfect 90-degree angle.
Q4: Why Do 11 Gauge Square Tubes Sometimes Crack During Fabrication?
If a 3.0mm tube cracks during secondary bending or drilling, it is usually due to excessive strain hardening at the factory. If the steel is overworked to create very sharp corner radii, it loses its ductility and becomes brittle. A balanced corner radius prevents this issue.
Q5: What Is Internal Scarfing, And Why Does It Matter For 3.0mm Tubes?
Internal scarfing is the process of removing the inner weld bead created during ERW. For an 11 gauge tube, if the factory leaves a jagged bead or cuts too deeply into the 3.0mm wall while removing it, it creates a stress concentration point. Under heavy load or vibration, the tube can crack from the inside out along this seam.
Q6: Can I weld 11 gauge steel without pre-heating?
Yes — in most cases. Standard 11 gauge carbon steel tubing (such as ASTM A500 Grade B) has a Carbon Equivalent Value (CEV) below 0.45, so it can be welded without pre-heating using normal MIG/GMAW settings. Two precautions matter at this thickness: keep heat input low to avoid burning through the 3.0 mm wall, and remember that cold-formed corners are harder than the base steel. For high-strength grades, thick welds, or low-temperature service, follow the pre-heat requirements in AWS D1.1 before welding.